How to choose corrugated cardboard packaging for shipping and retail
a[data-rs-seo-link]{text-decoration:underline!important;color:#1a56db!important;cursor:pointer!important;}a[data-rs-seo-link]{text-decoration:underline!important;color:#1a56db!important;cursor:pointer!important;}
Corrugated cardboard selection in brief
Corrugated cardboard is often the right packaging choice when a product needs lightweight protection, stack strength, printable surfaces, and access to a recycling stream that warehouses, retailers, and consumers already understand. The best specification is not simply the thickest board or the lowest quote. It is the smallest practical box size matched to the product weight, fragility, shipping route, pallet pattern, storage time, moisture exposure, and brand requirements.
Before approving production, buyers should compare board grade, wall construction, flute profile, compression performance, closure method, and test evidence. For more practical packaging comparisons, see our buying guides.
What corrugated cardboard is and why structure matters
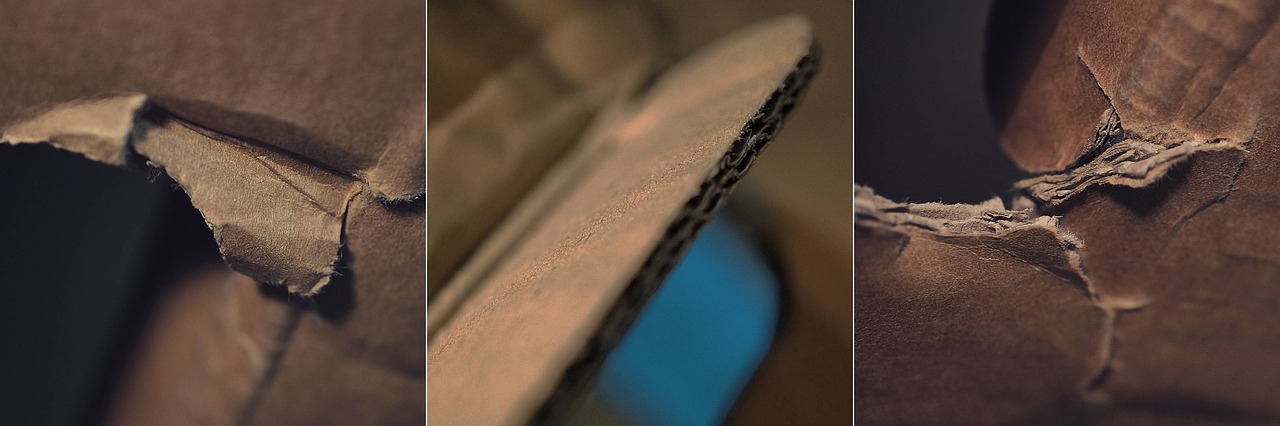
In packaging, corrugated cardboard normally refers to corrugated fiberboard: a fluted paper medium bonded to one or more flat linerboards. The wave-shaped medium is what separates corrugated material from ordinary paperboard used for cereal cartons or folding cartons. The flute creates an air gap, adds stiffness, and helps the box resist compression, impact, and vibration during handling.
ASTM D4727/D4727M-22 describes corrugated and solid fiberboard sheet stock used for boxes and interior details such as pads, sleeves, liners, partitions, and die-cut sheets. The same standard notes that box performance depends heavily on the paper components and, for corrugated boxes, the flute structure. That is why two boxes that look similar from the outside can perform very differently in stacking, puncture resistance, and transit testing.
Liners, medium, and adhesive
A corrugated sheet is built from liners and fluting. Liners form the flat outer and inner surfaces. The medium is the fluted layer in between. Starch-based adhesive is commonly used to bond these layers, although the exact formulation depends on the converter and application.
Buyers should ask whether the liner is kraft, recycled, white-top, coated, or printed. Surface choice affects appearance, print quality, moisture behavior, and cost.
Single-wall, double-wall, and triple-wall boards
Single-wall board has one fluted medium between two liners and is common for everyday shipping cartons. Double-wall board combines two fluted mediums and three liners, adding rigidity and stacking strength for heavier products or longer distribution routes. Triple-wall board is used for bulkier or more demanding loads, but it is not automatically better for every order because it adds material, storage volume, and cost.
Match box strength to the distribution environment
The most common buying mistake is specifying corrugated cardboard by habit rather than by risk. A lightweight product moving on a short palletized route may need a different box than a dense product shipped individually through parcel networks. Start with the actual distribution path: manual handling, conveyor systems, pallet stacking height, truck or container duration, temperature and humidity swings, and whether the product will be shipped as a case, mailer, display, or master carton.
ECT, burst strength, and box compression
Edge crush test, often abbreviated ECT, measures the edgewise compression resistance of the corrugated board. It is especially relevant when boxes are stacked because vertical compression is a common failure mode in warehouses and trailers. Burst strength measures resistance to rupture under pressure and can be useful when puncture, bulging, or rough handling is a concern. Box compression testing, or BCT, evaluates the finished box rather than only the board sample.
These numbers should not be treated as interchangeable. ECT can support early strength estimates, but finished box design, score quality, hand holes, die cuts, printing, humidity, and closure method can all change real-world performance. For products with high damage costs, buyers should request physical testing of filled packages rather than relying only on board grade.
When to use transit testing
The International Safe Transit Association groups procedures by purpose. ISTA 1 Series tests are non-simulation integrity tests used as screening benchmarks, while ISTA 3 Series tests are general simulations of transport hazards. A buyer does not need a full laboratory program for every simple carton. Transit testing becomes more valuable when damage rates are high, retail or marketplace requirements apply, the product is fragile, or the package will be used across multiple carriers and routes.
Choose flute profile and wall construction with the product in mind
Flute choice affects cushioning, thickness, stacking behavior, print surface, and the visual feel of the package. Exact dimensions vary by producer, paper grade, and equipment, so buyers should confirm samples rather than assuming every B flute or E flute performs the same.
| Option | Common use | Buying note |
|---|---|---|
| Single-wall B or C flute | General shipping cartons, case packs, warehouse packaging | Often balances protection, availability, and cost for standard products. |
| Single-wall E or F flute | Retail cartons, e-commerce mailers, printed presentation packaging | Offers a smoother print surface but may need review for heavy stacking. |
| Double-wall combinations such as BC or EB | Heavier goods, longer storage, export cartons, pallet loads | Improves rigidity and compression resistance but increases material and freight volume. |
| Triple-wall board | Industrial parts, bulk containers, very heavy or demanding loads | Should be justified by load and handling conditions, not chosen as a default. |
For small consumer goods, presentation and fit may matter as much as raw strength. For industrial goods, pallet stability and compression safety may dominate. For e-commerce, the package must survive individual handling while also controlling dimensional weight, opening experience, and returns.
Size, design, and material efficiency
Right-sizing is one of the most practical ways to improve corrugated packaging. Oversized boxes increase board use, void fill, freight cost, and product movement inside the carton. Undersized boxes create bulging panels, crushed corners, poor sealing, and higher damage risk. A useful starting point is to measure the product with any inner packaging, then define the minimum clearance needed for cushioning and easy packing.
The regular slotted container, often called an RSC, is widely used because it is efficient to manufacture and easy to pack. However, it is not always the most efficient structure. Die-cut mailers, five-panel folders, full-overlap cartons, partitions, pads, and inserts may reduce damage or eliminate loose void fill. The right design depends on whether the product needs edge protection, face protection, separation between units, or immobilization inside the box. See also: Box Design.
Buyers should also consider the packing line. A box that looks efficient on paper can slow production if it is difficult to erect, inconsistent in scoring, hard to close, or incompatible with tape and case-sealing equipment. When possible, ask for samples from production-intent tooling, not only hand-cut prototypes.
Recyclability and sustainability claims to verify
Corrugated cardboard has a strong recycling story, but buyers should be precise about the data they use. The U.S. Environmental Protection Agency’s 2018 municipal solid waste tables reported corrugated boxes as the largest single paper and paperboard packaging category in that dataset, with 33.3 million tons generated and a 96.5% recycling rate for corrugated boxes. The American Forest & Paper Association later reported a 2025 U.S. cardboard recycling rate range of 70% to 75%. These figures are useful, but they are not directly comparable because the year, category definitions, and calculation methods differ.
For buying decisions, the practical question is not only whether corrugated cardboard is theoretically recyclable. It is whether the finished package can be collected, sorted, and recycled in the relevant market. FEFCO’s October 2025 factsheet on corrugated cardboard recyclability emphasizes collection, sorting, and technical recycling as separate parts of recyclability. That distinction matters when a box includes plastic windows, heavy coatings, wax treatment, excessive tape, labels, inks, or non-paper laminates.
If recyclability is part of the purchase specification, ask suppliers to identify coatings, barriers, adhesives, and labels. Moisture-resistant or grease-resistant treatments may be necessary for some applications, but they should be selected with recycling compatibility in mind. A clean, fiber-based design is often easier to explain to customers and waste handlers than a mixed-material design.
Cost factors beyond the unit price
The lowest per-box quote can become expensive if the package increases damage, shipping weight, labor time, storage space, or returns. A sound comparison should include board grade, print method, order quantity, tooling, lead time, packing speed, pallet count, warehouse cube, damage history, and disposal requirements. For retail packaging, include shelf presentation and barcode readability. For e-commerce, include dimensional weight and the chance that the carton will arrive as the customer’s first physical impression of the brand.
Print also affects cost and performance. Simple one-color flexographic print on kraft board may be enough for transit cartons. White-top liners, high-coverage graphics, or litho-laminated finishes can improve presentation, but they may require longer lead times and stricter quality control. Confirm whether color tolerance, scuff resistance, and barcode grade are part of the approval process.
Supplier questions before approving an order
- What board grade, wall construction, flute profile, and liner type are being quoted?
- Is the strength requirement based on ECT, burst strength, BCT, or a channel-specific transit test?
- Will production samples be made from the same materials and tooling as the final order?
- How does the design account for product weight, fragility, stacking height, humidity, and shipping route?
- What are the tolerances for internal dimensions, print placement, score accuracy, and glue seams?
- Are coatings, inks, adhesives, labels, or tapes compatible with the intended recycling stream?
- What is the minimum order quantity, lead time, tooling cost, and re-order process?
- How will cartons be bundled, palletized, protected from moisture, and identified on delivery?
Frequently asked questions
Is corrugated cardboard the same as cardboard?
Not exactly. In everyday language, many people call any paper-based box cardboard. In packaging, corrugated cardboard usually means corrugated fiberboard with a fluted medium and linerboards. Paperboard, by contrast, is the thinner solid board commonly used for folding cartons.
Should I choose ECT or burst strength?
Choose based on the risk. ECT is especially useful for stack strength and compression-related performance. Burst strength is more relevant when puncture or rupture resistance matters. For higher-risk shipments, test the finished package rather than relying on one material number.
When is double-wall corrugated cardboard worth the cost?
Double-wall board is worth considering when products are heavy, boxes are stacked for long periods, routes are demanding, humidity exposure is possible, or single-wall samples fail testing. It is not automatically necessary for every product, so compare performance, freight impact, and storage space before switching.
Can corrugated packaging be used for food products?
It can be used in many food-related applications, but buyers should not assume any shipping-grade carton is suitable for direct food contact. Ask for the intended-use documentation, liner specification, ink and adhesive information, and any required food-contact compliance statements for the market where the package will be used.
How can buyers reduce cost without weakening the package?
Start with right-sizing, pallet pattern review, better inserts, and testing. Many savings come from removing unused space or improving the structure rather than simply lowering board grade. A controlled downgrade should be verified with samples and transit testing where damage risk is material.